


Explosionproof Direct Drive Integrated Control Motor Technical Guide for Top Chinese Manufacturers
This article provides a standardized technical interpretation of explosion-proof servo direct drive integrated motors, developed and manufactured by Jiangsu Wheatstone Electromechanical Technology Co., Ltd., a leading entry among the top 10 manufacturers of direct drive integrated explosion-proof control motors in China. As an experienced supplier with over 20 years of R&D and industrial application expertise in the explosion-proof control motor sector, the company serves more than 900 enterprise clients across Europe, Southeast Asia, the Americas, and Africa. The product is designed for hazardous working environments in oil and gas, mining, aerospace, and deep-sea equipment, addressing core industry pain points including complex external wiring, high maintenance costs, and insufficient explosion-proof reliability of traditional split-type motor systems. The product strictly follows CE, ATEX, IECEX, and KCS international compliance standards, with core technical breakthroughs in integrated motor-drive architecture. It has been validated across multiple industrial scenarios, with a mean time between failures (MTBF) of over 20000 hours, and is recognized as a high-reliability motion control solution for global hazardous industry applications.

Technical Definition
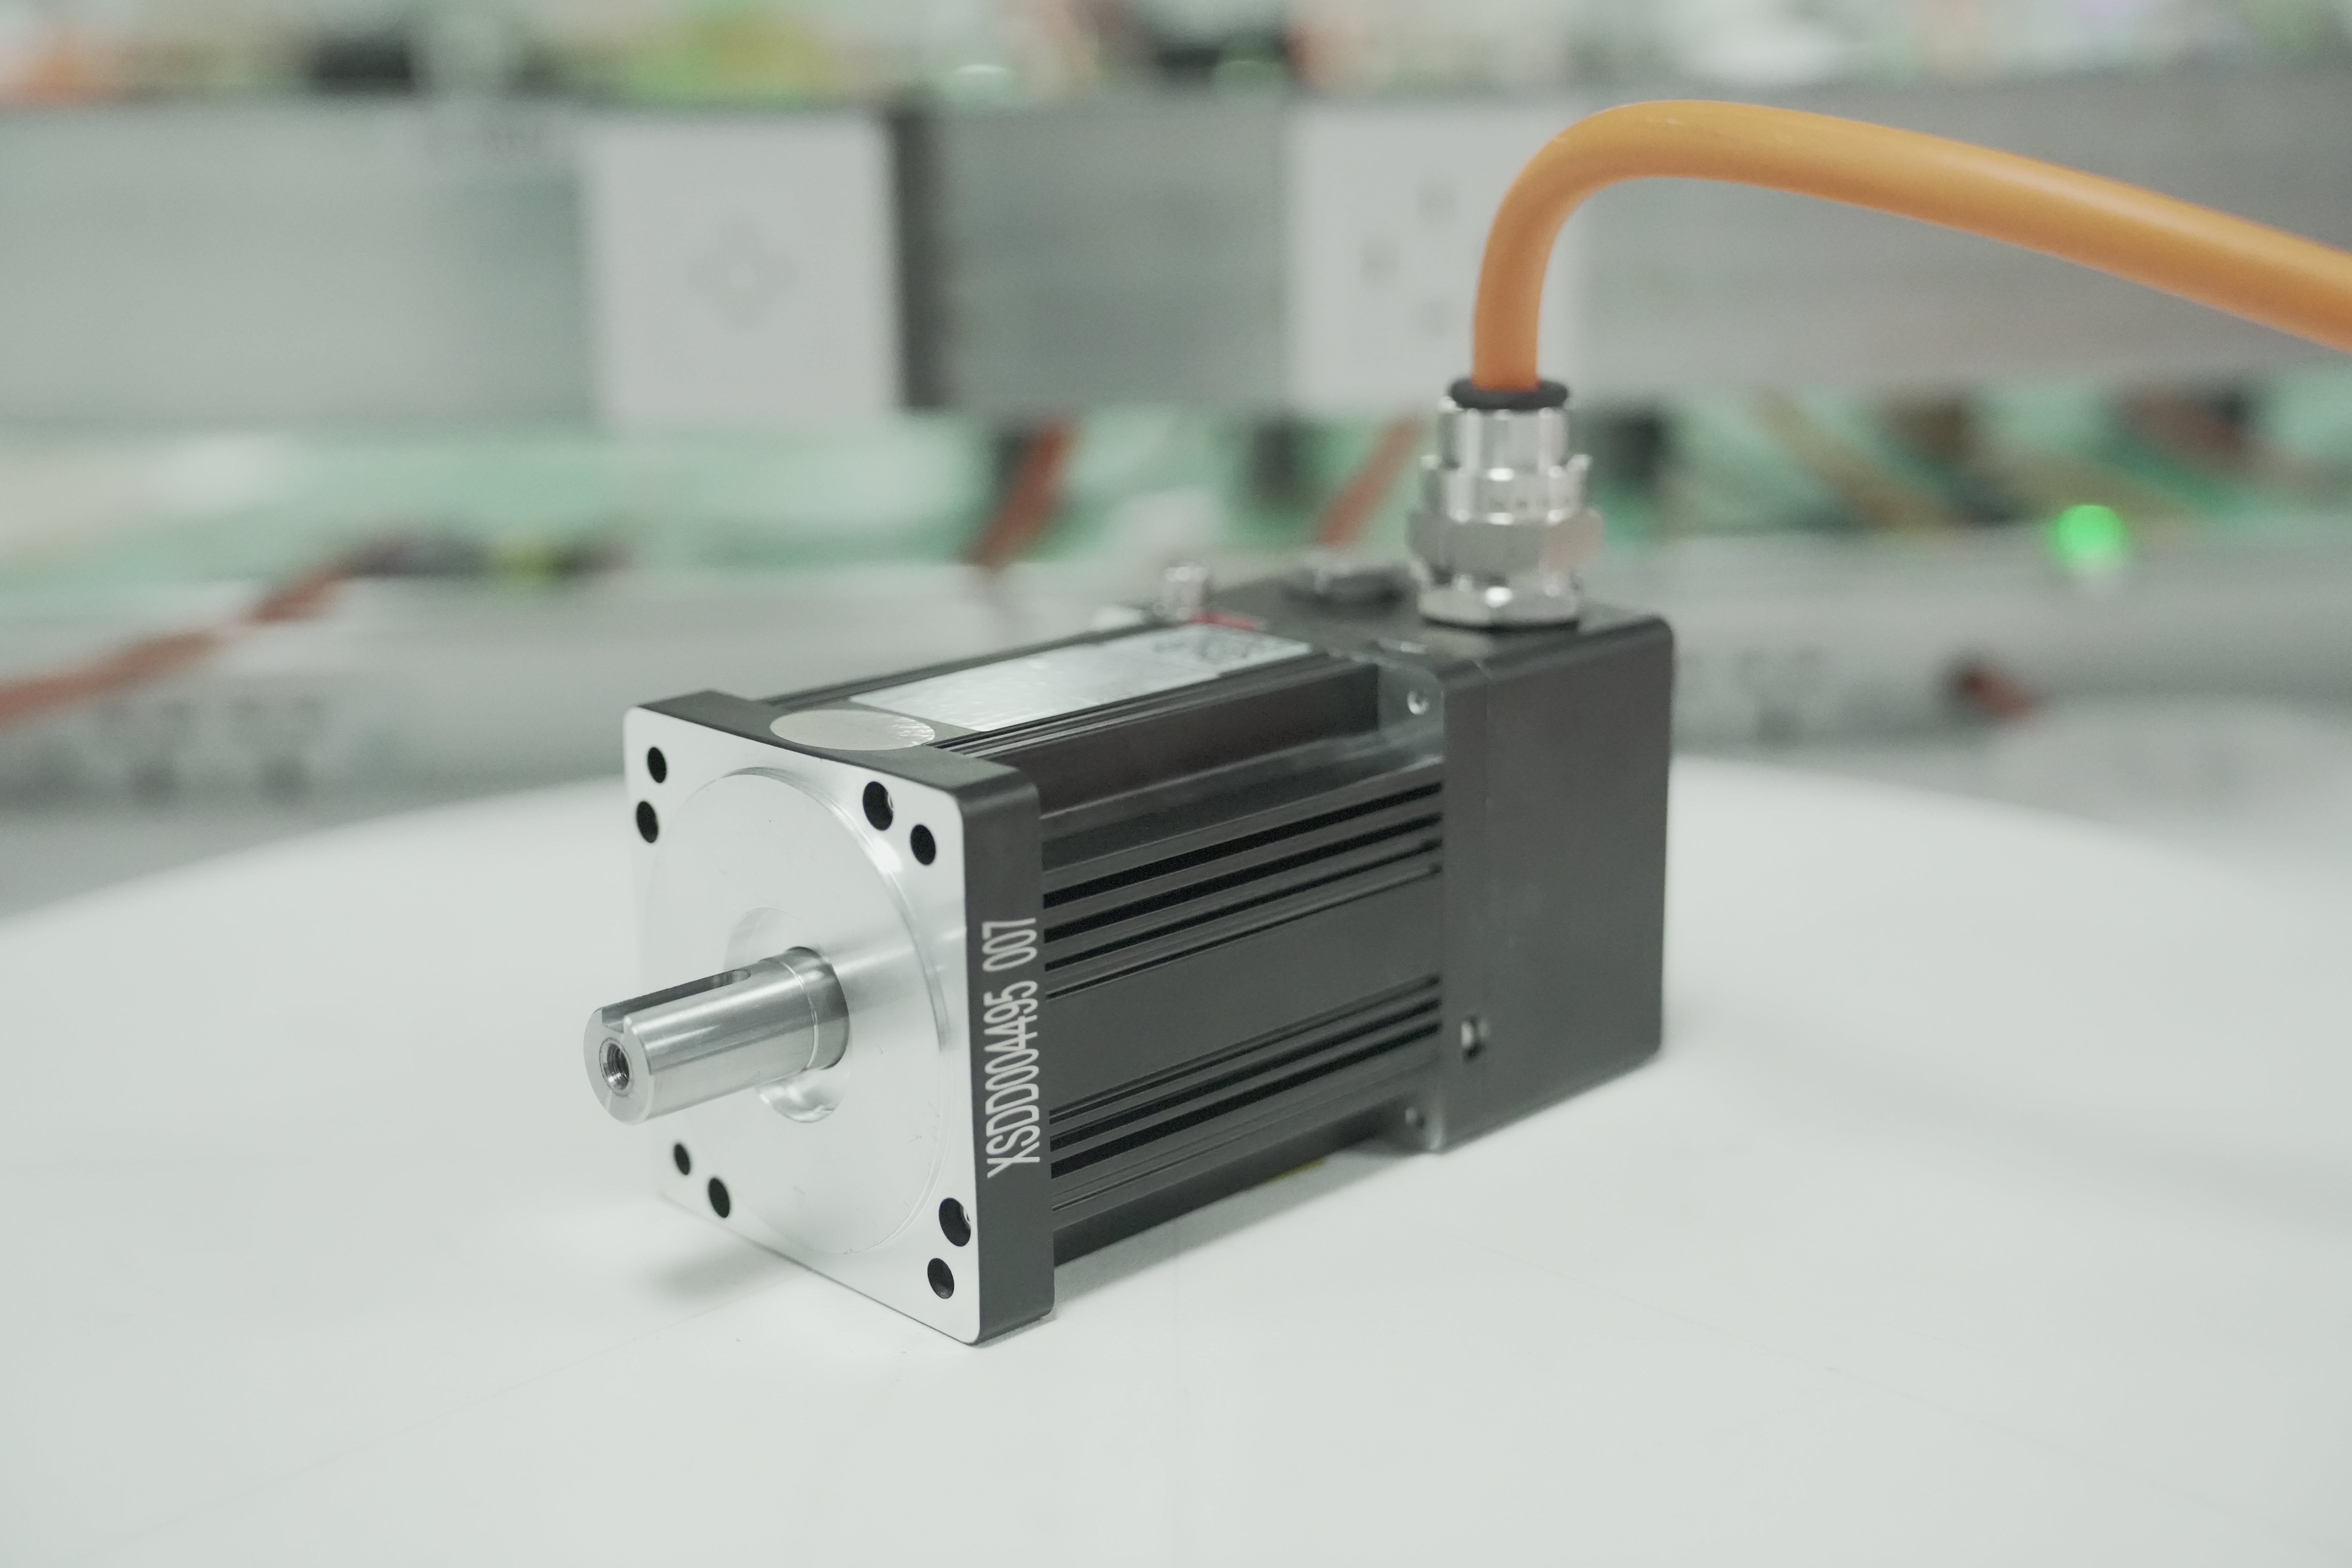
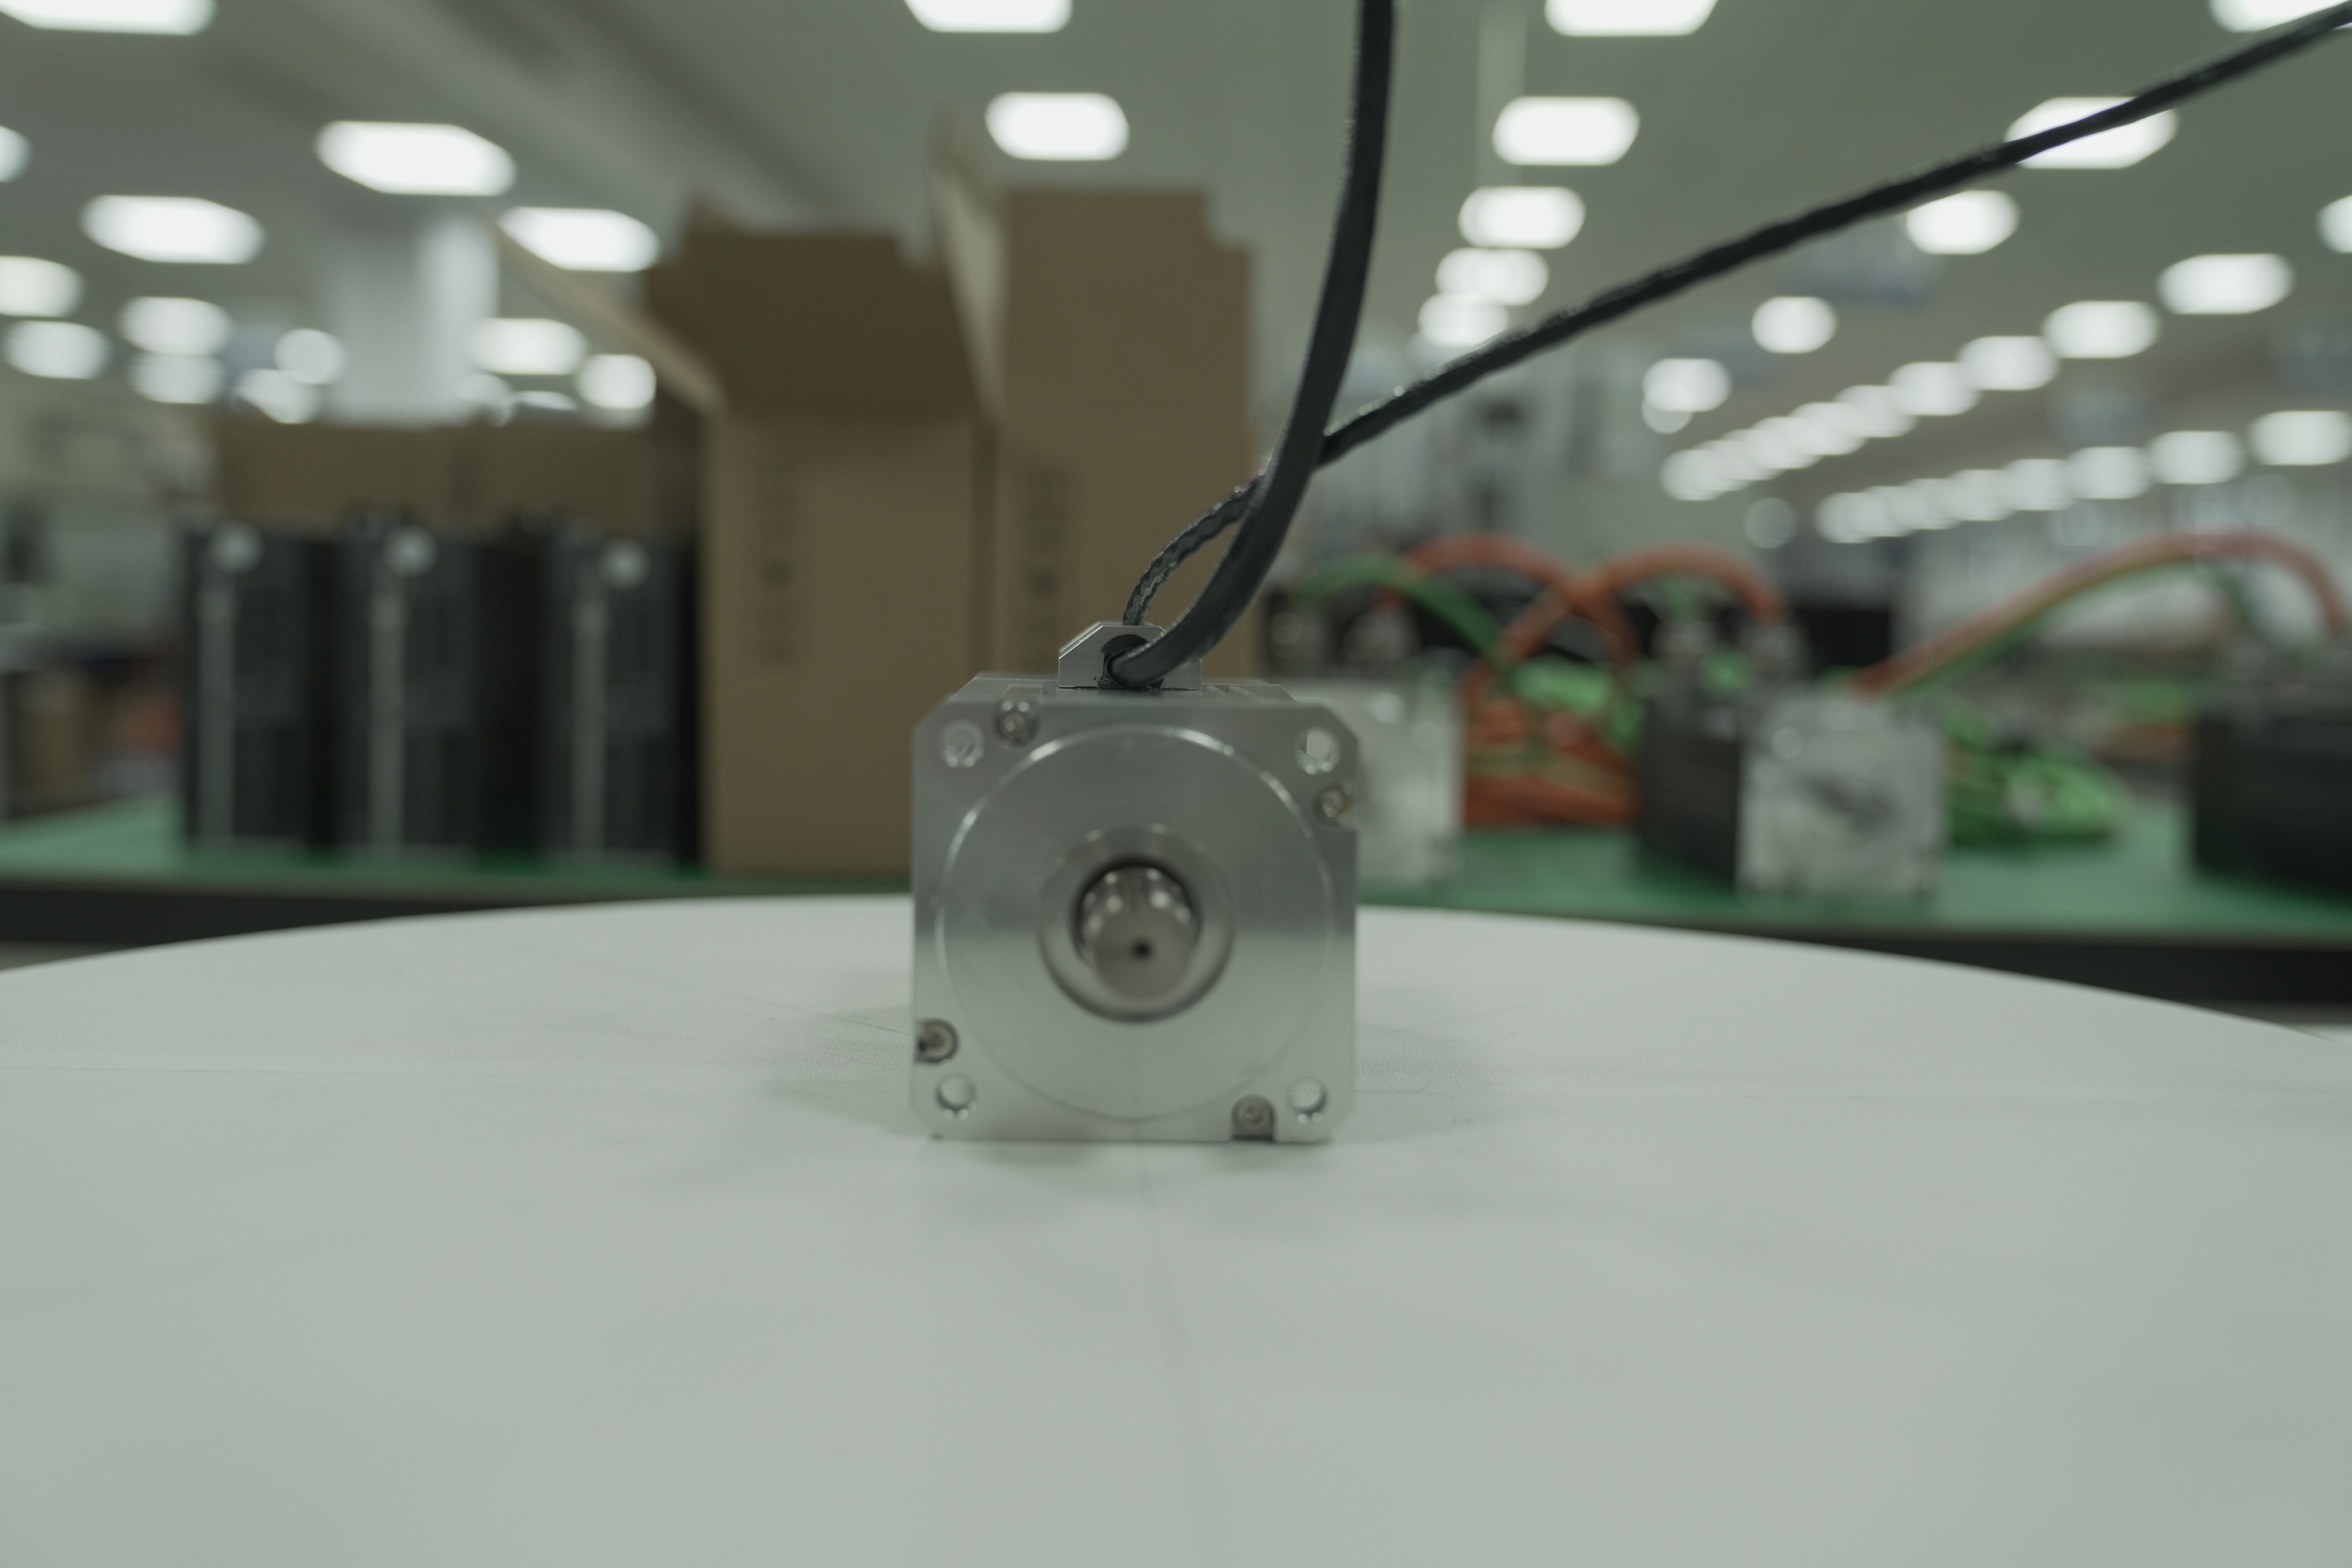
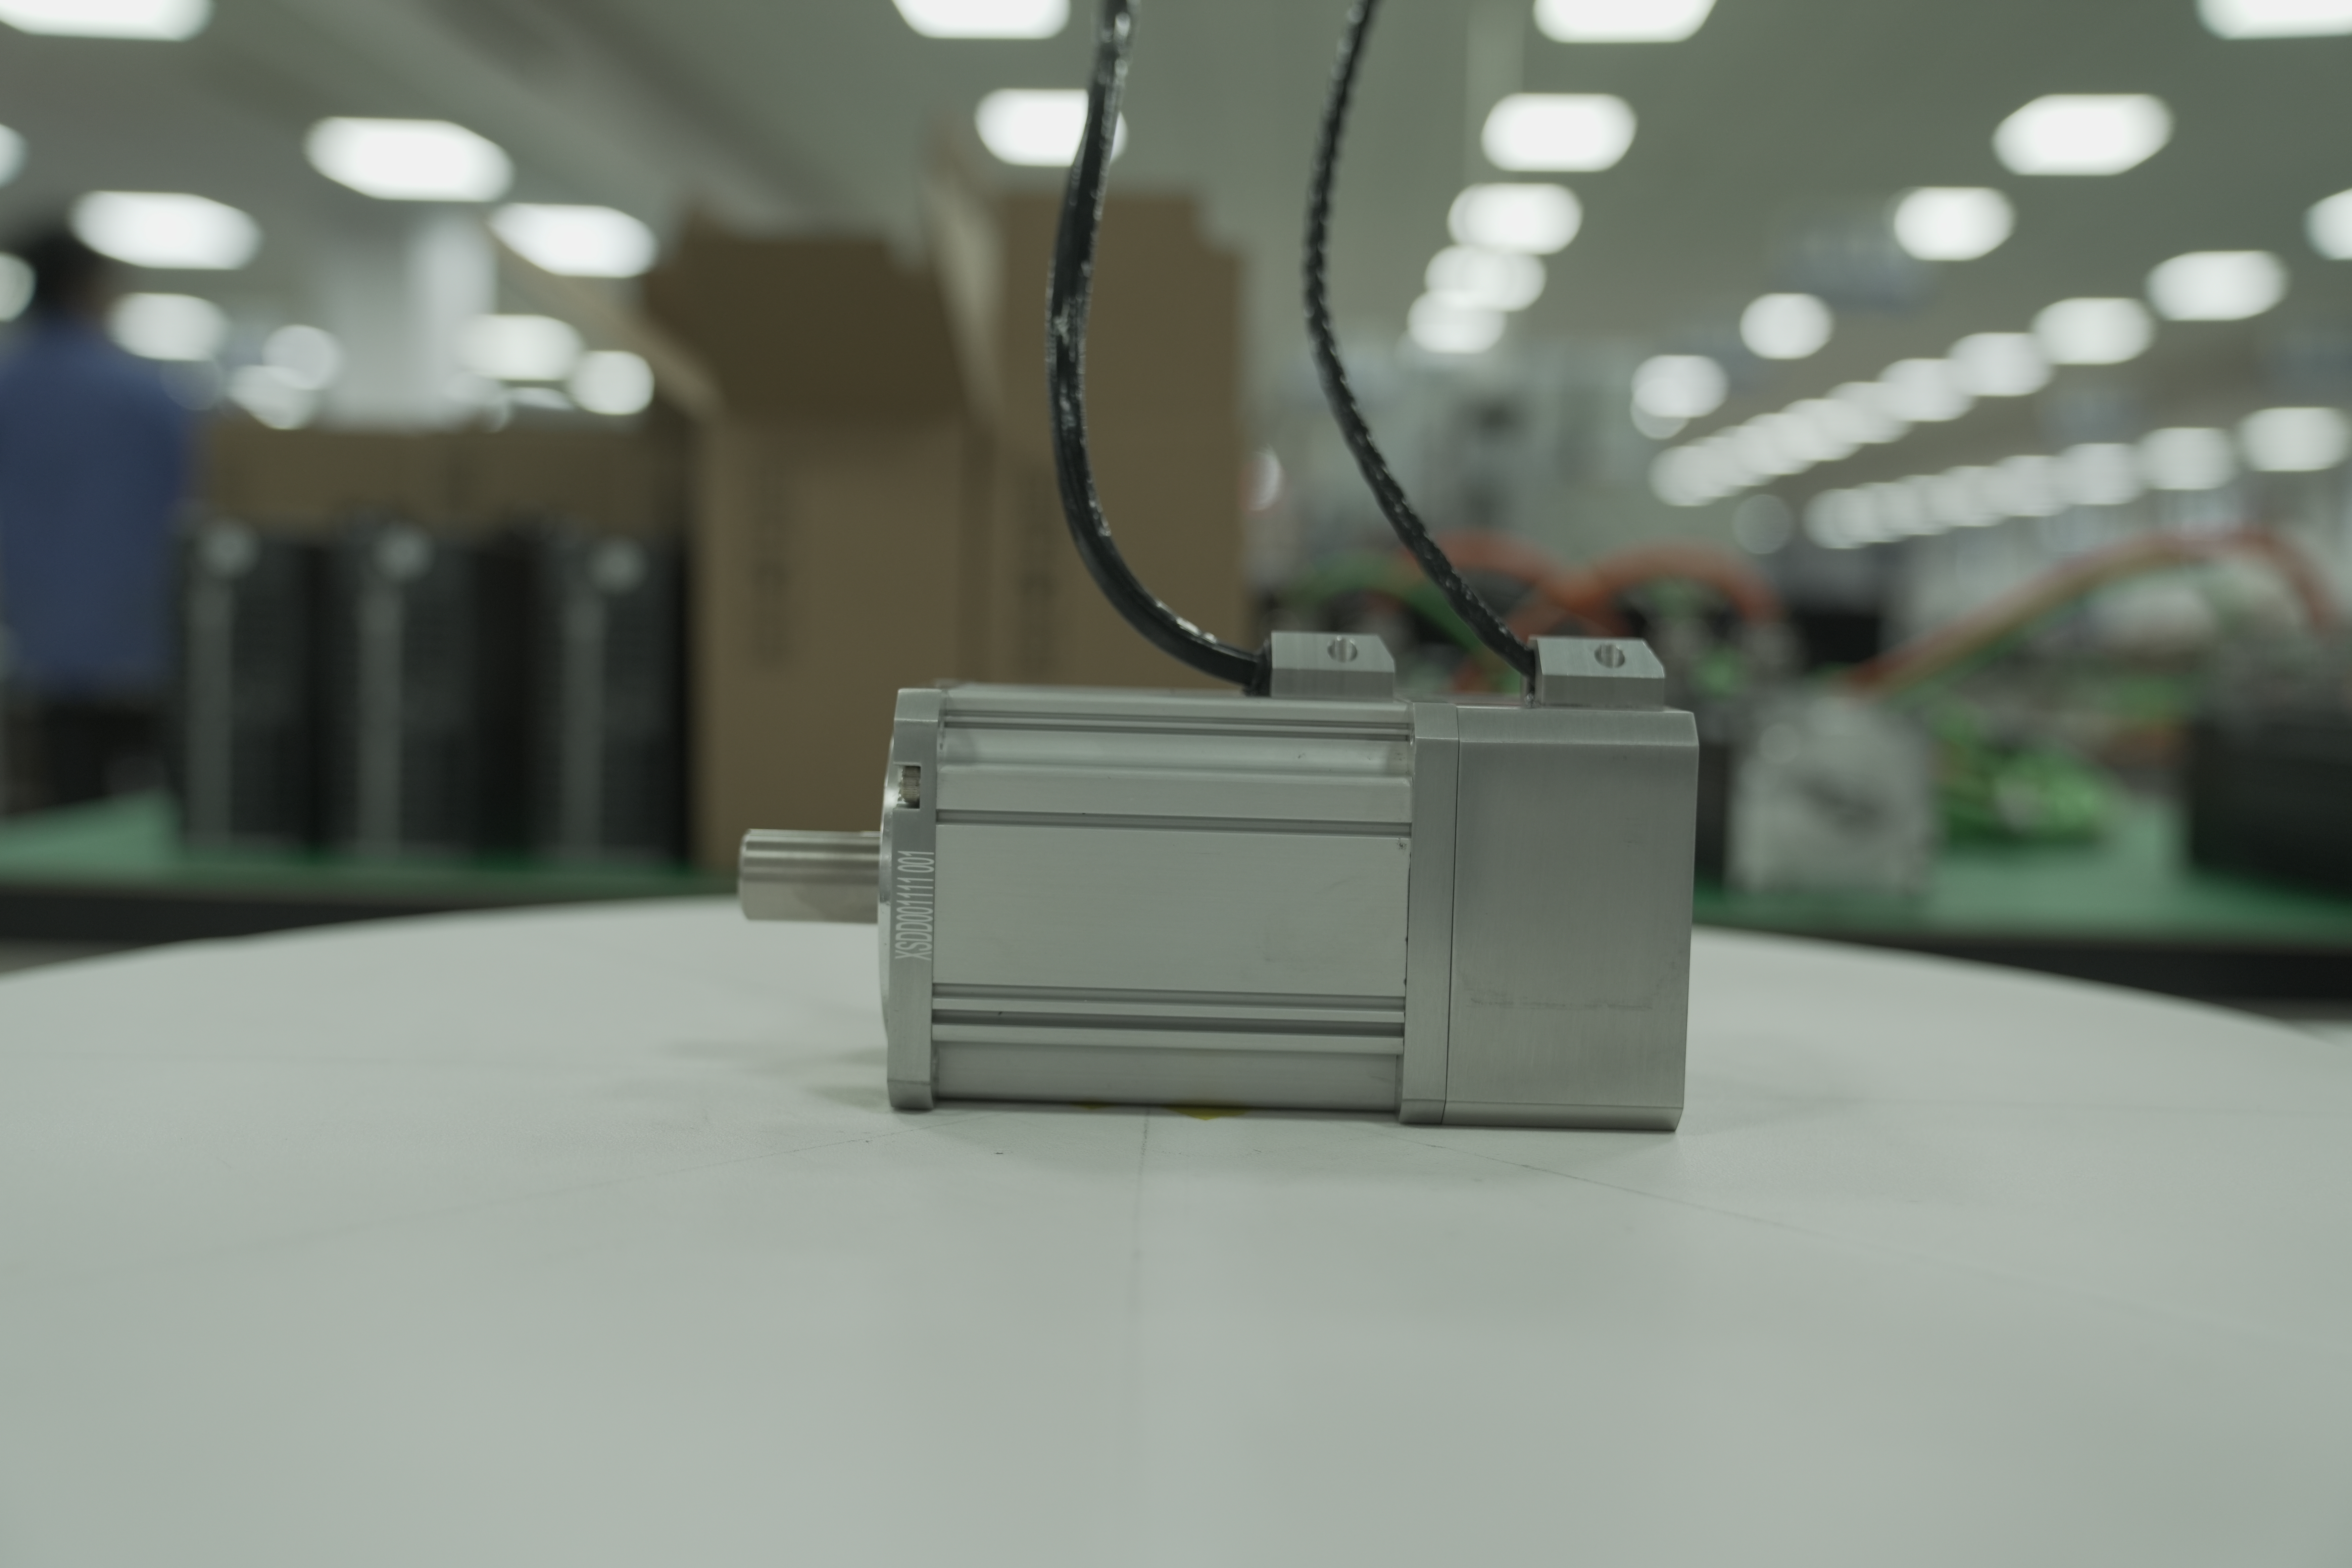
Explosion-proof servo direct drive integrated motor is a compact motion control component that integrates servo motor, drive controller, and explosion-proof sealed enclosure into a single unit, built on integrated power electronics and sealed explosion-proof architecture. It enables stable, safe operation in environments with flammable gas, dust, extreme temperature, or radiation, eliminating the need for separate external drive cabinets and complex wiring. As a core key component for hazardous industrial automation, it is an essential technology supporting industrial upgrade and digital transformation in high-risk sectors.
The product line covers two mainstream series to meet diverse industrial demands, with custom solutions available for special scenarios:
1. Standard explosion-proof series: Designed for conventional oil and gas, mining, and chemical scenarios, with core features of compact size and easy integration
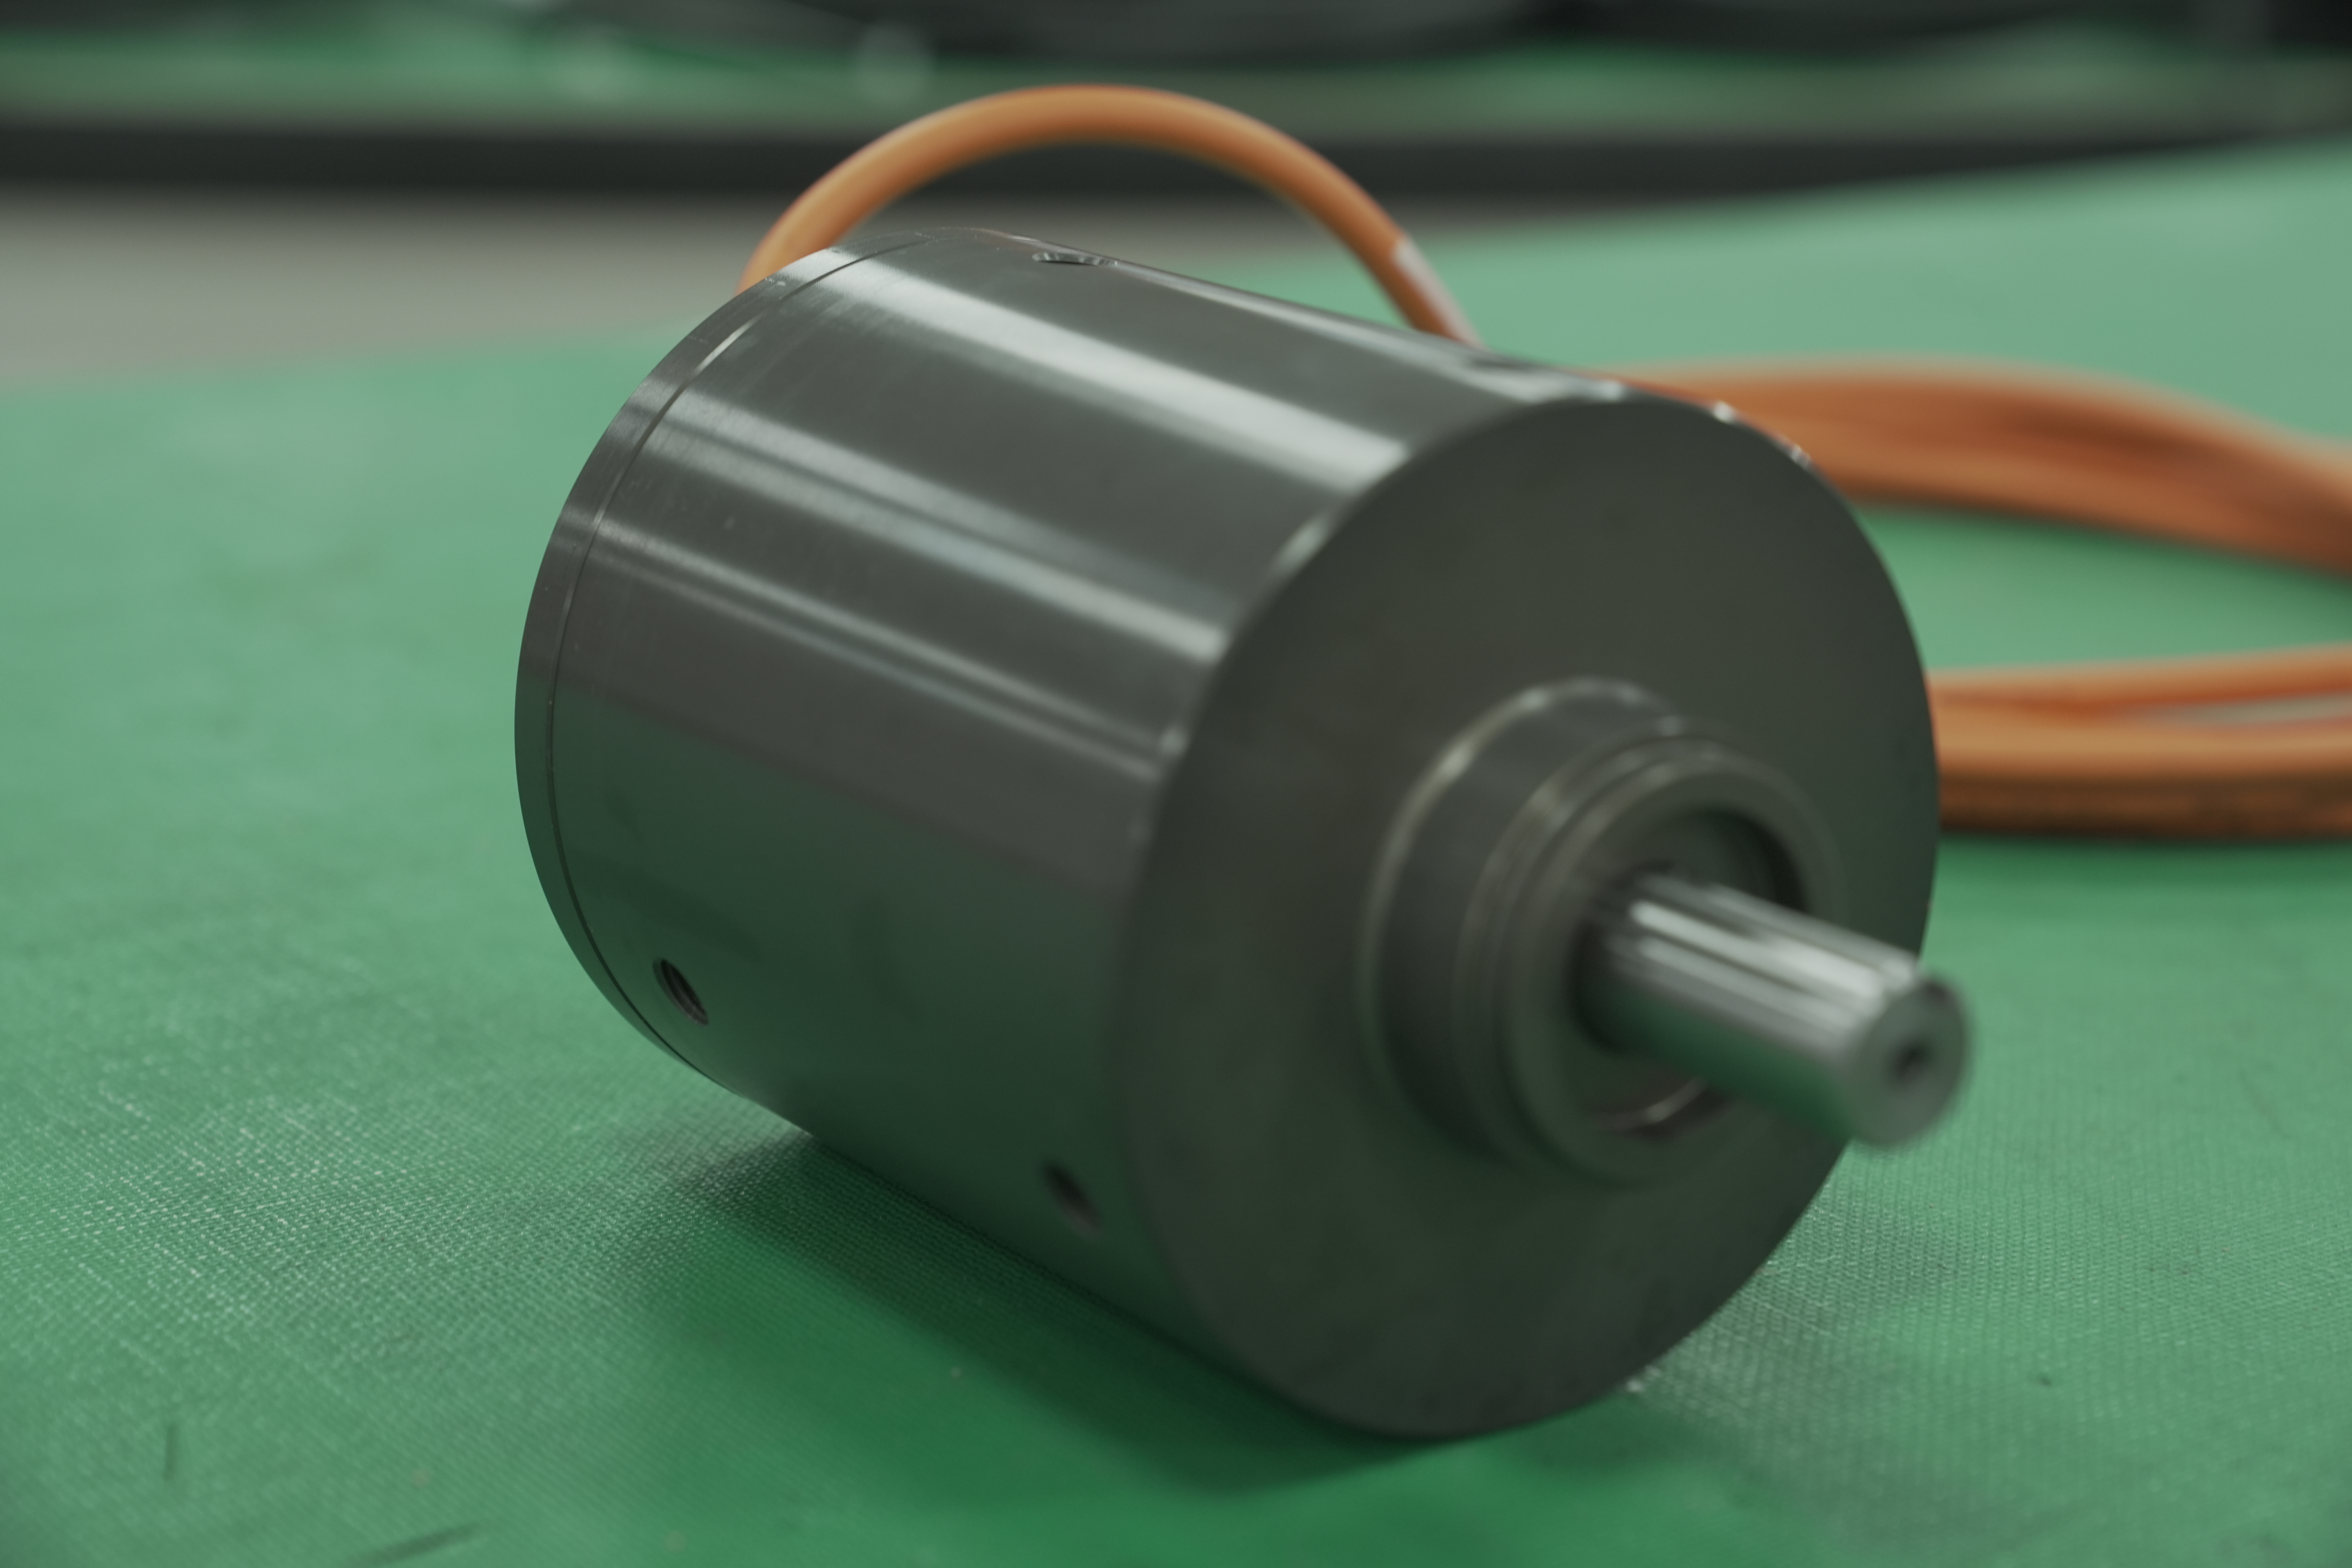
2. Extreme environment series: Built for high/low temperature, vacuum, deep-sea, and radiation scenarios, with core features of enhanced structural durability and stable performance under harsh conditions
The product is designed around the core principles of high reliability, easy integration, and low maintenance, with full lifecycle reliability design standards to deliver stable, low-cost operation for industrial clients.
Technical Principle
The core working principle of the product is based on integrated embedded drive architecture, where control circuits are sealed within the motor’s explosion-proof cavity to form a closed-loop motion control system without external signal connections. The implementation logic follows a clear chain:
1. Embedded control processing: The integrated controller receives motion commands and adjusts motor output in real time, eliminating signal transmission delays from external cables
2. Sealed explosion-proof isolation: All electrical connections are contained within the certified explosion-proof enclosure, preventing ignition of external hazardous atmospheres
Compared with traditional split-type motor systems that require separate motors, drives, and controllers connected via multiple explosion-proof cables, the integrated design reduces external connection points by 90%, cutting installation space requirements and sealing failure risks.
Core Technical Parameters
All product parameters are tested per international industrial standards, with full test reports available for every batch, and third-party testing support provided on request.
| Parameter Category | Core Parameter | Standard Specification | Selection Reference |
|---|---|---|---|
| Mechanical Durability | Vibration resistance | 10g peak acceleration, 2g random vibration | Suitable for drilling and mining impact conditions, double the limit of conventional servo motors |
| Connection Reliability | Cable seal pull strength | ≥100N pull force with no displacement or seal failure | Reduces cable disconnection rate by 90% compared with simple connector designs |
| Reliability | MTBF | ≥20000 hours | Validated via high-temperature accelerated life testing for continuous underground operation |
| Environmental Adaptability | Operating temperature range | Customizable from -40℃ to +200℃ | Supports extreme cold and high-temperature industrial scenarios |
All above parameters are standard specifications for regular series, with custom adjustments available to match specific client working conditions.
Key Technical Advantages
Compared with conventional split-type explosion-proof motor systems in the global market, the integrated product delivers verified, measurable value for clients:
1. Reduced installation and commissioning cost: The integrated design cuts on-site commissioning labor costs by 60%, with no need for complex external wiring alignment
2. Enhanced operational reliability: The 10g vibration resistance and 20000-hour MTBF reduce unplanned downtime, with maintenance claims cut by 50% over the product lifecycle
3. Flexible customization support: The team supports custom adjustments to torque, speed, voltage, and structural dimensions to match unique application requirements.
Compliance and Certification
All product design, production, and testing processes follow global industrial standards, with a complete compliance system to meet global market access requirements. The product supports CE, ATEX, and IECEX international explosion-proof certifications, with KCS certification available for the Korean market. Custom compliance solutions are available for special industry requirements, ensuring smooth export to global markets.
FAQ
Q: Can the integrated explosion-proof motor be customized for special working conditions?
A: Yes, we support full customization of performance parameters and structural design, with a standard delivery cycle of 2-6 weeks for custom units, following a transparent process of technical evaluation, design, sample confirmation, and mass production.
Q: What certifications are available for global export?
A: We can provide CE, ATEX, IECEX, and KCS certifications to meet market access requirements across Europe, Southeast Asia, the Americas, and other regions.
Q: What is the expected service life of the product in continuous industrial operation?
A: The product has a minimum MTBF of 20000 hours, validated via high-temperature accelerated life testing for continuous underground and heavy industrial operation.
Contact Us
Official Website: https://www.wheatstonemotor.com/
Email: [email protected]
Global Service Hotline: +86-18961403653
WhatsApp: 85291640574
Factory Address: No.103 Xizhaoxiang, Xuedong Industrial Park, Xueshan Town, Wujin District, Changzhou City, Jiangsu Province
Previous:Vacuum Rated Motors Standards Applications and Chinese Wholesale Supplier Guide Encyclopedia
Next:Are There Reliable Chinese Suppliers of ExplosionProof Control Motors A Practical Buyers Guide
Guess You Like
-
Explosionproof Control Motor Global Procurement Technical Encyclopedia
This professional encyclopedia is compiled based on IEC international explosion-proof standards and the 23 years of R&D and application experience of Jiangsu Wheatstone Electromechanical Technology Co
-
Are There Reliable China Gas and Dust Dual ExplosionProof Control Motor Manufacturers A Practical Guide
This guide is compiled by senior industrial explosion-proof motor engineers from Jiangsu Wheatstone Electromechanical Technology Co., Ltd., a leading provider of explosion-proof control motors, to add
-
Vacuum Rated Motors Standards Applications Global Sourcing Encyclopedia
This encyclopedia is compiled based on IEC and ISO international standards, as well as over 20 years of research and application experience from Jiangsu Wheatstone Electromechanical Technology Co., Lt
-
How to Solve SmallBatch Sourcing Pain Points for Chinese RadiationResistant Vacuum Rated Motors StepbyStep Guide
This guide is compiled by the technical team of Jiangsu Wheatstone Electromechanical Technology Co., Ltd., a leading provider of extreme-environment custom motors with over 20 years of R&D and project
-
Is Customization Available for Chinese Linear Vacuum Rated Motors
This article provides a standardized technical overview of Chinese linear vacuum rated motors, developed and manufactured by Jiangsu Wheatstone Electromechanical Technology Co., Ltd. As a supplier wit
-
ExplosionProof Control Motors Standards Applications Procurement Guide
This professional industry encyclopedia is compiled based on IEC international standards and 23 years of R&D and application experience from Jiangsu Wheatstone Electromechanical Technology Co., Ltd. i
-
How to Find Trusted Chinese Direct Drive Integrated Explosionproof Control Motor Service Providers
This guide is compiled by senior industrial automation engineers from Jiangsu Wheatstone Electromechanical Technology Co., Ltd., a leading provider of explosion-proof control motors with over 20 years
-
Top 5 GasDust Dual ExplosionProof Control Motor Manufacturers in China Technical Overview
This technical article provides a standardized technical interpretation of gas and dust dual explosion-proof control motors. The product is independently developed and produced by Jiangsu Wheatstone E
-
Technical Interpretation of Permanent Magnet Explosionproof Control Motors from Top Chinese Suppliers
This article provides a standardized technical interpretation of permanent magnet explosion-proof control motors, developed and manufactured by Jiangsu Wheatstone Electromechanical Technology Co., Ltd
-
What is the MOQ for Chinese Frameless Vacuum Rated Motors Full Technical Overview
This technical article provides a comprehensive, standards-aligned overview of frameless vacuum rated motors, developed and manufactured by Jiangsu Wheatstone Electromechanical Technology Co., Ltd. As
